
Exploring the Reaction Conditions for 3-(Trifluoromethyl)acetophenone Synthesis
A detailed analysis of temperature, pressure, and mass parameters for multi-step organic synthesis.
Key Insights
- Diazotization Conditions: 3-(Trifluoromethyl)aniline reacts with 15% H₂SO₄ and NaNO₂ at low temperature (0–5°C) under atmospheric pressure to form the diazonium salt.
- Oxime Formation & Hydrolysis: Subsequent reaction with CuSO₄·5H₂O and acetaldoxime forms an oxime intermediate; hydrolysis with 30% HCl at elevated temperatures (50–100°C) efficiently converts the intermediate to 3-(trifluoromethyl)acetophenone.
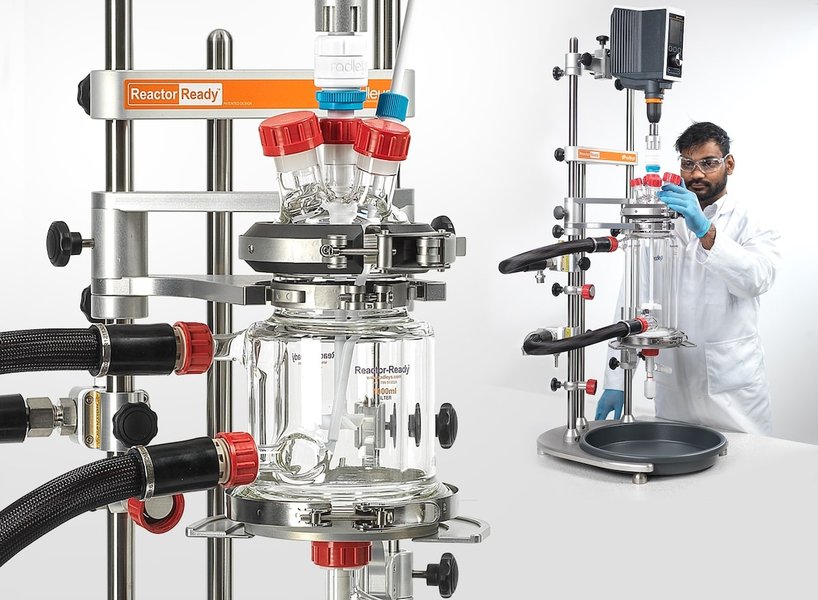
- Mass & Reactor Setup: Stoichiometric quantities adjusted to scale, a jacketed/slurry reactor made of glass or stainless steel is recommended to handle different temperature zones safely.
Detailed Reaction Overview and Conditions
The synthesis of 3-(trifluoromethyl)acetophenone from 3-(trifluoromethyl)aniline is achieved via a multi-step process that involves controlled diazotization followed by an oxime formation, and concluding with hydrolysis to furnish the ketone. This method demands precise control over reaction parameters at each stage to optimize the yield and purity of the final product.
Step 1: Diazotization
Initially, 3-(trifluoromethyl)aniline is dissolved in 15% H₂SO₄ to provide an acidic medium necessary for protonation of the amino group. Sodium nitrite (NaNO₂) is then added slowly to generate nitrous acid (HNO₂) in situ. The nitrous acid reacts with the protonated amine to form an arenediazonium salt. For safety and optimal stability, this exothermic reaction should be conducted at low temperatures ranging from 0°C to 5°C with atmospheric pressure.
Key Parameters for Diazotization
| Parameter | Condition | Purpose |
|---|---|---|
| Temperature | 0–5°C | Prevents decomposition of the diazonium salt; Aids controlled nitrosation |
| Pressure | Atmospheric | Standard lab conditions |
| Mass Ratios | Stoichiometric/ Slight excess of H₂SO₄ and NaNO₂ | Ensures complete conversion to diazonium salt |
Step 2: Neutralization and Stability
Following the formation of the diazonium salt, sulfamic acid is introduced to neutralize any excess HNO₂, in addition to stabilizing the rapidly formed diazonium intermediate and preventing side reactions.
Step 3: Reaction with CuSO₄·5H₂O and Acetaldoxime
The diazonium salt is subsequently treated with copper(II) sulfate pentahydrate (CuSO₄·5H₂O) in the presence of acetaldoxime. Copper(II) sulfate acts as an efficient catalyst which facilitates the coupling reaction, leading to the formation of an intermediate oxime. This reaction is typically performed at a slightly elevated temperature, commonly around room temperature to 30°C, and under atmospheric pressure.
Parameters for Oxime Formation
| Stage | Temperature | Pressure | Notes |
|---|---|---|---|
| Oxime Formation | 20–40°C (room temperature region) | Atmospheric | Catalytic action by CuSO₄·5H₂O ensures efficient reaction |
Step 4: Hydrolysis to Form 3-(Trifluoromethyl)acetophenone
The final step is the hydrolysis of the oxime intermediate with 30% HCl. This acid-catalyzed hydrolysis is typically conducted at a higher temperature, ranging between 50°C and 100°C. Temperatures in this region help in accelerating the conversion of the intermediate into 3-(trifluoromethyl)acetophenone. Maintaining an atmospheric pressure remains sufficient during this process, though the system may be slightly pressurized if reflux conditions are applied within a closed reactor.
Hydrolysis Parameters
| Parameter | Condition | Purpose |
|---|---|---|
| Acid Concentration | 30% HCl | Ensures complete hydrolysis of the oxime intermediate |
| Temperature | 50–100°C | Facilitates rapid conversion under reflux conditions |
| Pressure | Atmospheric (or slightly elevated under reflux) | Standard conditions unless reaction scaling demands a closed system |
Reactor and Mass Considerations
Reactor setup: To achieve precise temperature control across these varied steps, a jacketed reactor or a reactor with precise temperature control and stirring is highly recommended. Materials of construction for the reactor should be-resistant to strong acids, typically glass-lined or stainless steel, ensuring safe handling of corrosive reagents and conditions.
Mass Ratios: Proper stoichiometric ratios should be maintained starting with 3-(trifluoromethyl)aniline in a near equimolar ratio with the acid and sodium nitrite during diazotization. Additional reagents such as sulfamic acid and acetaldoxime are often used in slight excess to drive the reactions to completion. Details in established literature suggest that a slight excess of the diazotizing agent (NaNO₂) and acetaldoxime catalysis by CuSO₄·5H₂O are optimal. The final hydrolysis step should be monitored to ensure complete conversion, with mass yields calculated based on starting material purity and reaction loss.
Visualizing the Process
To help conceptualize the multi-step synthesis and the reaction conditions, the following visual tools offer a comprehensive representation. The radar chart below depicts the variation in key reaction parameters (temperature, pressure, and stoichiometric precision) across the different steps, while the mindmap illustrates the overall reaction scheme.
Safety, Handling, and Usage Considerations
It is paramount to adhere to strict safety protocols when handling highly reactive intermediates like diazonium salts and powerful reagents such as strong acids and nitrites. Protective equipment (gloves, goggles, lab coats) and proper ventilation must be employed. Additionally, any deviations from the recommended temperature ranges or stoichiometric calculations could result in undesired side reactions or thermal runaways. Consider consulting detailed material safety data sheets (MSDS) and literature for detailed hazard profiles of each reagent.
The synthesis process must be scalable with special attention to exothermic events during the diazotization. Reactor design should account for efficient heat dissipation, and volume controls must allow for controlled addition of reagents. The use of a jacketed reactor or a reactor with in-built temperature control is advised to maintain homogeneity and avoid localized hot spots.
Optimizing Reaction Efficiency
Thorough optimization of reaction parameters such as reagent purity, reaction times, and stoichiometric precision can maximize the overall yield. The intrinsic variability of diazotization reactions makes it crucial to maintain rigorous environmental controls. Monitoring through inline sensors for temperature and pH ensures that each stage of the reaction proceeds as expected. Efficiency can be further improved by conducting small-scale tests to calibrate the reactor before full-scale synthesis.
FAQ
What is the ideal temperature for the diazotization step?
The diazotization is best performed at 0–5°C to avoid decomposition of the diazonium salt and minimize side reactions.
Why is sulfamic acid used in the reaction?
Sulfamic acid is added to neutralize excess nitrous acid and stabilize the diazonium intermediate, thereby reducing side reactions during the process.
What role does copper(II) sulfate play in the synthesis?
Copper(II) sulfate pentahydrate catalyzes the formation of the oxime intermediate by facilitating the coupling reaction between the diazonium salt and acetaldoxime.
What is the significance of using 30% HCl in the final step?
The 30% HCl concentration provides a strong acidic environment necessary for efficient hydrolysis of the oxime intermediate to yield 3-(trifluoromethyl)acetophenone.
References
- 3-(Trifluoromethyl)aniline - Wikipedia
- Chemical Hazards and Data - NOAA
- Reactions Involving Arenediazonium Salts - Lumen Learning
- Diazotisation Reaction Mechanism - Organic Chemistry Portal
- 3-(Trifluoromethyl)aniline Data - PubChem
Recommended Further Queries
 assets.thermofisher.com
Last updated March 31, 2025