
Catalytic Conversion of Sugars to Ethanol with Manganese Sulfate Catalyst
Exploring a Chemical Approach to Biofuel Production
Key Takeaways
- Catalyst Properties: Manganese sulfate acts as an effective transition metal catalyst offering Lewis acidic and potential redox properties in a sulfate-fortified acid medium.
- Mechanistic Pathways: The process involves dehydration, bond cleavage/rearrangement, and reduction steps leading to the formation of ethanol directly from sugars.
- Operational Advantages: The chemical catalytic method provides a streamlined alternative to fermentation, potentially offering improved efficiency, broader feedstock compatibility, and continuous operation.
Introduction
The catalytic conversion of sugars to ethanol using manganese sulfate represents a significant divergence from traditional fermentation-based biofuel production. While biological fermentation relies on yeast and other microbial processes, this chemical method offers a direct approach to convert simple sugars into ethanol, bypassing many of the limitations associated with biological systems.
Manganese sulfate, a relatively inexpensive and readily available transition metal salt, plays a crucial role in this process. With its dual role as a Lewis acid and potential redox agent, manganese sulfate activates the sugar molecules and assists in their transformation into ethanol under controlled conditions. This alternative route promises energy efficiency and the potential for operating under a broad range of reaction temperatures and mediums.
Scientific Background and Rationale
Traditional Bioethanol Production vs. Chemical Catalysis
Conventional ethanol production relies on biological fermentation where microbes such as yeast ferment sugars to produce ethanol. Though effective, fermentation is limited by factors including substrate specificity, product inhibition, and slower conversion rates. In contrast, the chemical catalytic conversion of sugars to ethanol using manganese sulfate allows a direct route that is independent of biological constraints. This not only expands the variety of sugars that can be utilized (including glucose, fructose, sucrose, and mannose) but also provides a controlled chemical environment that can be precisely manipulated to enhance conversion efficiency.
Role of Manganese Sulfate in the Conversion Process
Manganese sulfate functions primarily as a catalyst in the sulfate-fortified acid medium used for converting sugars to ethanol. The catalyst exhibits the following properties:
Lewis Acid Behavior
The manganese ion, in its sulfate form, interacts with hydroxyl groups in the sugar molecules. This form of Lewis acid activation reduces the energy barrier for dehydration reactions by facilitating the removal of water. This is the first critical step that allows the sugar molecules to form reactive intermediates.
Potential Redox Activity
Although less emphasized than the Lewis acid mechanism, manganese sulfate can also engage in redox reactions under certain conditions. The possibility of manganese cycling between oxidation states may assist in hydrogen transfer or reduction steps, ultimately aiding in the final conversion to ethanol.
Mechanistic Details of the Catalytic Conversion
The pathway from sugar to ethanol using manganese sulfate involves several key steps. These include sugar dehydration, bond cleavage, rearrangement, and, if necessary, a reduction step. Each stage is essential for trimming the carbon chains in the sugar to yield ethanol, a C2 molecule.
Step 1: Dehydration of the Sugar
The initial reaction in the conversion process is the dehydration of the sugar. Under catalytic conditions, manganese sulfate activates the sugar, facilitating the removal of a water molecule. This dehydration is crucial for forming reactive intermediates, such as open-chain derivatives or even species resembling 5-hydroxymethylfurfural (HMF) in some cases. The loss of water prepares the sugar molecule for further transformation steps.
Step 2: Bond Cleavage and Rearrangement
Once the sugar has been dehydrated, the resulting intermediate undergoes C–C bond cleavage and rearrangement. Manganese sulfate catalyzes this process by lowering the energy barrier required for breaking bonds within the molecule. The cleavage typically produces smaller carbon fragments. Through rearrangement, these fragments reorganize into species that are closer in structure to ethanol.
Step 3: Hydrogen Transfer and Reduction
The final transformation often includes a hydrogen transfer or reduction step. In some reaction setups, additional hydrogen donors are introduced, or conditions are set to generate hydrogen in situ, facilitating the reduction of the intermediate molecules into ethanol. The manganese catalyst may assist in this hydrogen transfer, completing the conversion process.
It is important to note that while the overall scheme of the reaction is straightforward, the precise mechanistic details depend on several factors, including temperature, pressure, solvent environment, and the concentrations of catalysts and acids.
Reaction Conditions and Technical Considerations
The catalytic conversion of sugars requires careful control of reaction parameters to achieve high efficiency and selectivity. Below are the major reaction parameters:
Temperature and Pressure
Although the reaction can occur under a range of temperatures, most processes involving transition metal catalysts operate at moderately elevated temperatures. Typically, the reaction temperature can range from ambient conditions (0°C) to temperatures as high as 250°C. Some processes, however, may optimize conditions between 150°C to 250°C to drive dehydration and bond cleavage effectively. Pressure, too, may be controlled via closed systems like autoclaves to ensure phase homogeneity, especially when water is the primary solvent.
Acidic Medium and Catalyst Loading
The reaction medium is fortified with inorganic sulfates, including minerals such as cesium sulfate, magnesium sulfate, or other related salts. The acid component, often sulfuric acid, is adjusted to create an environment conducive to both dehydration and intermediate stabilization. Maintaining an optimal acid concentration is vital for suppressing side reactions that may lead to byproducts like levulinic acid, furfural, or polymeric humins.
Catalyst loading is another critical parameter. Adequate amounts of manganese sulfate must be introduced; however, too high a concentration can lead to unwanted side reactions or catalyst deactivation. The balance between maximizing activity and avoiding excessive side reactions is pivotal for the practical application of this process.
Solvent Selection and Additional Salts
Water is the most common solvent in such catalytic reactions, though alternative systems such as co-solvents or even ionic liquids may be employed. These alternatives can sometimes enhance catalyst performance and improve the solubility of sugar feedstocks. The presence of additional sulfate salts (e.g., potassium or sodium sulfate) can further modify the acid strength and ionic environment of the reaction, thereby influencing product yield and selectivity.
Process Integration and Continuous Operation
One of the advantages of the chemical catalytic pathway is the potential for continuous processing. Ethanol produced during the reaction can be removed by incorporating a distillation column within the reaction setup. In some advanced configurations, nitric acid injection aids in the continuous removal of ethanol, thereby shifting the reaction equilibrium and enhancing overall conversion.
Technical Comparison: Chemical Catalysis vs. Biological Fermentation
The distinct nature of the catalytic process using manganese sulfate sets it apart from traditional fermentation methods. The following table offers a comparison of key parameters between the two approaches:
| Parameter | Chemical Catalysis (Manganese Sulfate) | Biological Fermentation |
|---|---|---|
| Process Mechanism | Direct chemical conversion via dehydration, cleavage, and reduction. | Enzymatic conversion using microbes (e.g., yeast). |
| Catalyst/Enzyme | Transition metal salt (manganese sulfate) plus acid medium. | Yeast and other fermenting organisms. |
| Temperature Range | Can range from ambient to 250°C; typical optimization at 150-250°C. | Mild conditions (generally 30-40°C). |
| Reaction Time | Faster reaction rates under optimized conditions. | Slower, often several hours to days. |
| Feedstock Versatility | Utilizes a variety of sugars including glucose, fructose, sucrose, and mannose. | Primarily focuses on sugars that yeast can efficiently metabolize (mainly glucose, sucrose). |
| Process Integration | Potential for continuous operation with inline ethanol removal. | Typically a batch process with discrete fermentation cycles. |
This comparison highlights that while fermentation is well-established and operates under milder, biological conditions, chemical catalytic routes offer significant advantages in terms of speed, feedstock flexibility, and potential for streamlined continuous processing.
Challenges and Future Research Directions
Selectivity and Byproduct Formation
One of the central challenges in employing manganese sulfate catalysts for the conversion of sugars to ethanol is ensuring high selectivity for ethanol production. Side reactions remain a critical concern; unwanted byproducts such as levulinic acid, furfural, or polymeric humins can form if reaction conditions are not meticulously controlled. Understanding and mitigating these side reactions is a current focus of research.
Catalyst Reusability and Stability
For any catalytic system to be economically viable and sustainable, the catalyst must be stable over multiple cycles and, ideally, recyclable without significant loss of activity. Studies are ongoing to evaluate the longevity of manganese sulfate in these reaction conditions. The deactivation of the catalyst can occur due to the accumulation of byproducts or changes in its oxidation state, so formulating methods for regeneration and stabilization remains a critical research area.
Optimization of Reaction Parameters
Fine-tuning reaction parameters such as temperature, pressure, acid concentration, and catalyst loading is necessary to achieve maximum yield and selectivity for ethanol. Moreover, understanding the complex interactions between various sulfate additives and the acid medium is crucial. Advances in analytical techniques (e.g., NMR spectroscopy, GC-MS analysis) are leading to better insights into the mechanistic pathways, enabling more targeted optimizations.
Integration with Upstream and Downstream Processes
Integration with feedstock pretreatment and downstream product separation is essential for building a comprehensive and industrially scalable process. The compatibility of the catalytic reaction conditions with sugar feedstocks, and the efficiency of subsequent ethanol purification, determine the practical applicability of the process at a commercial scale.
Future research is expected to explore hybrid systems where catalytic methods could complement biological fermentation, blending the advantages of both approaches to maximize overall process efficiency.
Practical Implications and Potential Industrial Impact
The exploration of a catalytic pathway for converting sugars to ethanol using manganese sulfate is more than an academic exercise; it has substantial potential industrial implications. As industries push towards sustainable and efficient biofuel production methods, alternatives to fermentation offer flexibility and scalability.
The ability to process a wider range of carbohydrate feedstocks—not restricted to those that are easily metabolized by yeast—opens up possibilities for using non-traditional biomass sources. In addition, the rapid reaction times and potential for continuous processing could reduce reactor downtime and enable more efficient plant operations. These benefits, however, are balanced against technical challenges, such as ensuring catalyst longevity and product selectivity.
If ongoing research continues to address these challenges, the chemical catalytic process may serve as a complementary approach to established fermentation practices. This dual-method strategy would not only enhance overall production flexibility but also cater to regional differences in feedstock availability.
Case Study and Experimental Example
Experimental Setup and Observations
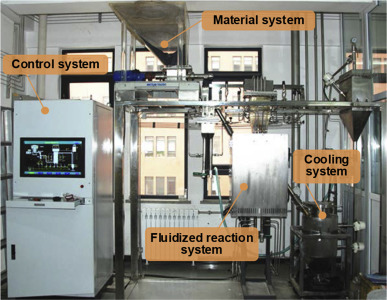
A notable experimental configuration involves a mixture containing manganese sulfate monohydrate, water, sulfuric acid, and a defined amount of glucose. In such setups, the manganese sulfate acts as the key catalyst facilitating the dehydration and rearrangement phases of the reaction. Controlled experiments indicated that even low concentrations of the catalyst (e.g., 0.0065 grams of manganese sulfate monohydrate) were effective in achieving noticeable ethanol yields.
The reaction mixture is typically heated within a defined temperature window (often between 150°C to 250°C) in the presence of an acid medium. As the reaction proceeds, ethanol is formed and can be continuously removed via distillation. This not only shifts the equilibrium in favor of product formation but also allows for a potential continuous process setup.
Performance Metrics and Efficiency
Quantitative analysis of the process shows that yields vary with adjustments in reaction conditions. High catalyst efficiency (in terms of turnover number) and minimal side reactions are the desired outcomes. For instance, careful balancing of the reaction parameters can minimize the formation of byproducts, resulting in a process that competes favorably with fermentation in terms of energy efficiency and throughput.
Advanced analytical techniques, such as gas chromatography and mass spectrometry, are employed to characterize the reaction products and optimize process parameters. This rigorous experimental evaluation is necessary to scale up the process from laboratory conditions to industrial applications.
Conclusion
The catalytic conversion of sugars to ethanol using manganese sulfate as a catalyst is a promising alternative to conventional fermentation methods. By leveraging the unique properties of manganese sulfate, including its ability to act as a Lewis acid and support redox reactions, this process outlines a direct chemical pathway for ethanol production. The method involves distinct sequential steps of dehydration, bond cleavage, rearrangement, and hydrogen transfer, all of which are critical for converting diverse sugar substrates into ethanol.
Despite notable benefits such as operational efficiency, versatility of feedstocks, and the potential for continuous processing, challenges remain. Issues concerning catalyst stability, selectivity, and byproduct formation require further research and optimization. Nonetheless, with ongoing investigations and advancements in mechanistic understanding, chemical catalytic conversion is poised to complement—and potentially enhance—traditional bioethanol production techniques.
In summary, while fermentation has been the traditional route for producing ethanol, the catalytic method using manganese sulfate opens up a new paradigm in biofuel technology, offering a pathway that is not only faster but adaptable to a broader spectrum of feedstock materials.
References
Related Queries for Further Exploration
Last updated February 19, 2025